THE OPTICAL FIBER CONNECTOR CERAMIC INSERT CORE

How to connect two optical fibers using a fiber optic connector

How to connect two optical fibers using a fiber optic connector

Fiber optic splicing is often the preferred way to connect two fiber optic cables because it has lower light loss (attenuation) and back reflection than connectorization. Fusion splicing and mechanical splicing are the two most common methods of fiber optic splicing. This involves aligning the two fiber ends and then fusing them together using heat or a specialized tool.

Read More
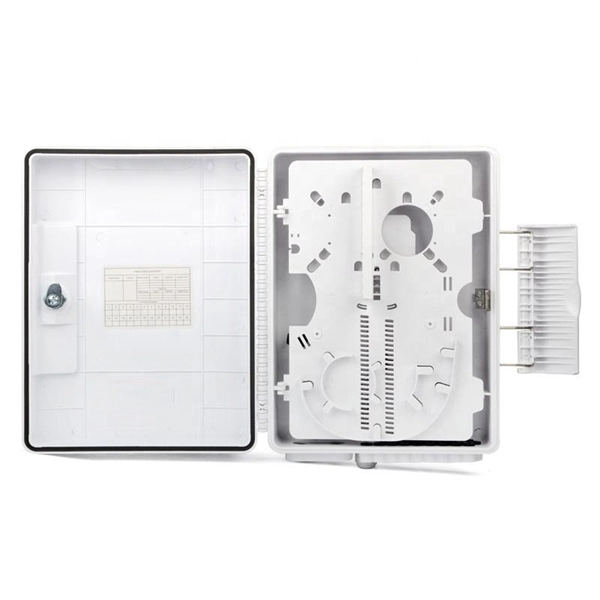
What is the diameter of the optical fiber core in millimeters

What is the diameter of the optical fiber core in millimeters

The diameters of the core and cladding play an important role in the specifications of the fiber optic cable. These dimensions directly impact performance, with smaller cores allowing long-distance transmissions. The standard cladding diameter for most optical fibers is 125um, and the standard outer protective layer diameter is 245um.

Read More
Om38 core optical fiber

Om38 core optical fiber

This fiber is a graded-index multimode fiber suitable for transmission speeds of up to 10 Gb/s. Multimode Fiber (MMF) has a core diameter, typically 50–100 micrometers, has ability to transfer multiple modes of light through the fiber core, uses lower-cost electronics (LED, VCSEL) operates at the 850 nm and 1300 nm wavelength and is used for short distance interconnections (up to 550m). Apart from the OM1 type, all of them are bending-optimized fiber incorporating technology to deliver enhanced macro-bending performance produced by a unique Plasma Chemical Vapor Deposition. Multimode fiber (MMF) optic cable carries multiple light modes (rays) simultaneously through a larger core diameter, typically 50 μm or 62. This larger core allows easier light injection and lower-cost optical sources (LEDs and VCSELs), making multimode fiber the cost-effective choice for.

Read More
Which ceramic core insert model is recommended

Which ceramic core insert model is recommended

Negative geometries prevail if up-milling is necessary, resulting in thick chips at the exit. Carefully select insert geometry, insert grade, insert shape (nose angle), insert size, nose radius and entering (lead) angle, to achieve good chip control and machining performance. PCD turning inserts are designed for high-performance turning of non-ferrous metals and composites. This includes aluminum alloys, brass, carbon fiber, fiberglass, composites and wear-resistant plastics. PCD is an advanced material, similar to CBN, made by bonding selected diamond particles. Second to only synthetic diamond on a scale of hardness, PCBN is characterized by its innate durability, as well d ceramic grades for HPT (Hard Part Turning). Sialon and whisker ceramics are viable alternatives for both turning and milling of heat-resistant super alloys (HRSA).

Read More

Get In Touch

Connect With Us

📱

Spain Office (HQ)

+34 936 214 587

🇪🇺

EU Technical Center

+49 89 452 38 217

📍

Headquarters (Spain)

Calle de la Tecnología 47, 08840 Viladecans, Barcelona, Spain